
 English
 Italiano
 Français
 Türkçe
Request quotation
Years ago, an operator could mount a single set of tools on a press brake and keep it running for days or even weeks. This represented the traditional view of manufacturing efficiency at its peak.
But the reduction of work orders and lead times has changed everything. A manufacturer might now have to execute 20 or more different tasks on the press brake within a shift. And many, if not all, of those workings require different tools, with all the changeover times that entails. Rarely can manufacturers afford such time and labor inefficiency.
Bending complex parts creates just as many challenges. With multiple bends requiring different sheet metal bending tool sets, complex parts require much more time for labor, setup, and dismantling.
Stage bending.
How can manufacturers achieve efficiency when forming complex parts or a series of different parts, all of which require a set of tools? In these cases, manufacturers turn to stage bending. With this method, multiple sets of tools (combinations of punches and dies) are arranged side by side on the press brake.
Operators can complete a complex part on one machine with a sole configuration. They can also use one configuration to bend a variety of parts, each using a combination of tools on a single press brake table.
This practice has become common in many workshops, where skilled press brake operators regularly work through various tooling setups.
Perfect sheet metal bending? Pay attention to the heights!
Then again, the task is not as simple as it seems. Arranging the tools in stage on the press brake is not enough!
A stage configuration must allow the operator to remove the part after each bend without damaging it. For stage bending to work, all tool sets must perform the intended task at the same height.
Given all this, how do press brake technicians and operators create these setups so that they can perform stage bending efficiently and effectively? There are several options.
Solution 1: shimming.
One possible option is shimming. This involves inserting a shim or riser under the tool so as to bring it to the same height as the others and avoid collisions. However, although seemingly simple, shims and risers can be difficult to calibrate and require considerable operator skill. In addition, it is possible that each tool may require ad hoc shimming, and this can give more problems than solutions.
Solution 2: Use tools from the same family.
Another possible option is to use tools that belong to the same type, for example, using dies and punches with the same bend angle. However, although more accurate and efficient than shimming, parts rarely have equal angles and openings. Consequently, this solution offers no flexibility in tool selection beyond a narrow circle.
Solution 3: Tools designed for stage bending.
The best choice, however, is to use tools designed to have the same height and work in stations, such as Eurostamp Tooling's ESH series (Eurostamp Same Height).
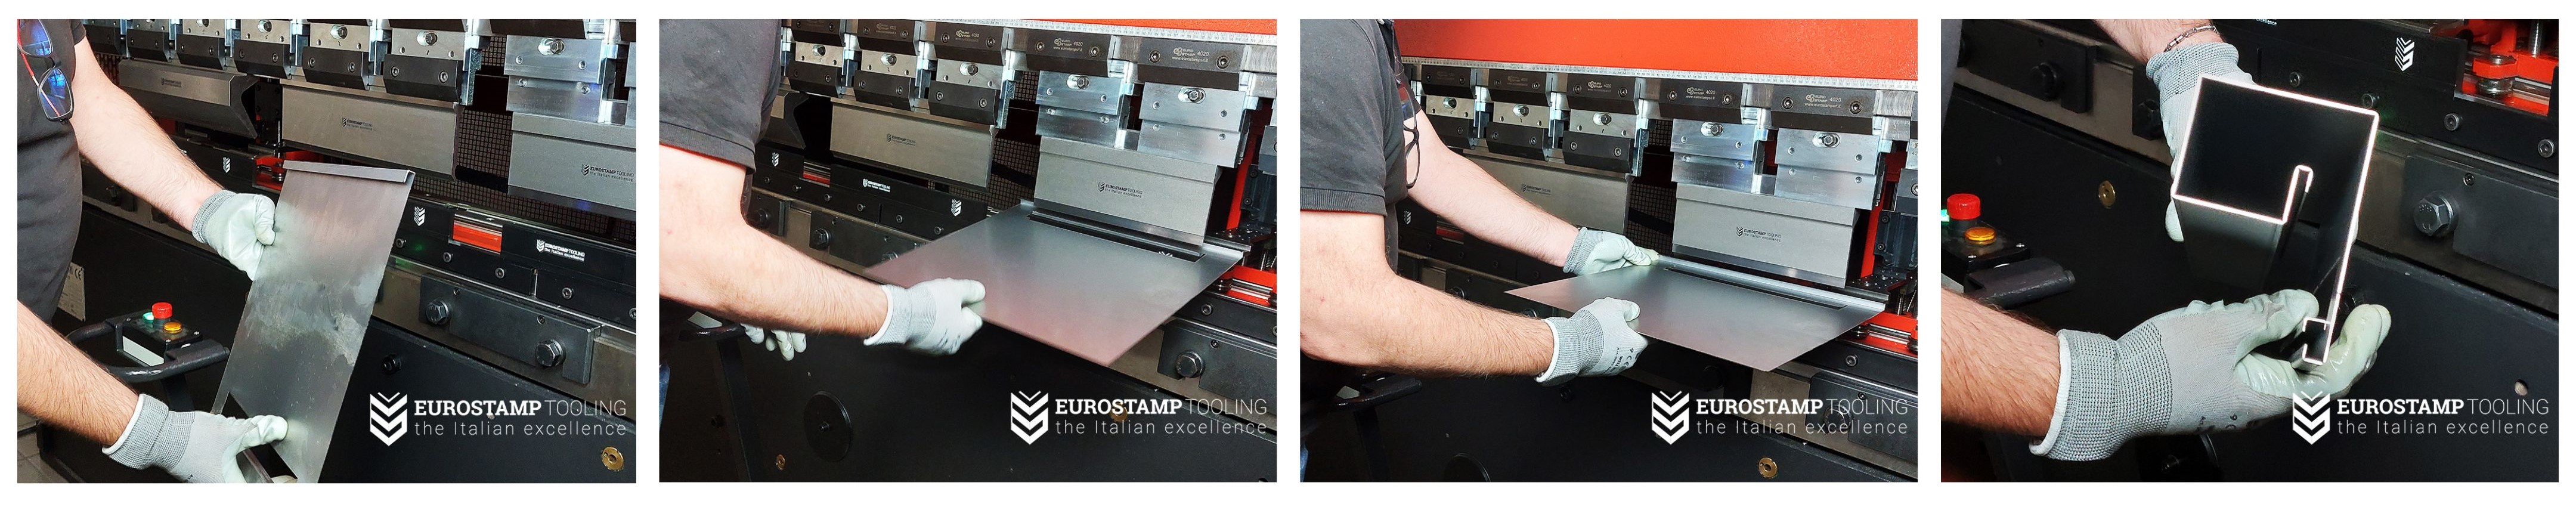
The best solution: ESH by Eurostamp Tooling.
Tools designed in this way eliminate the need for shims or risers and give maximum flexibility in use. Thanks to these tools, multiple groups of punches and dies can be set up on the same press, providing flexibility and speed to the operator. The latter, in this way, can move sequentially from one stage to another, handling one piece at a time.
When producing pieces that differ from each other or with very small batches, bending in stations with tools such as Eurostamp Tooling's ESH offers the best solution:
- allows for greater speed, reducing tool changeover times;
- allows greater flexibility, enabling the operator to work on different stages with parts that require very complex bending;
- allows the workshop floor to considerably reduce the number and variety of tools it needs to work with.
Moreover, they are tools machined from the best steel and with the best treatments to withstand wear and heavy duty work.
Therefore if, in modern press brakes, pressure control and management systems allow working in stages with extremely accurate 3-D simulations with respect to the bending sequence to obtain the final part, even with the help of systems that physically guide the operator from one station to another, even for older machines it is possible to have great advantages by working with tooling in stages, saving time, money, material handling and the amount of tooling required in the workshop.
Complex bending? Eurostamp Tooling can help you.
Eurostamp Tooling specialists are there to help press brake operators to choose the best solutions for flexibility, speed and savings. Staged bending with Eurostamp Tooling's ESHs offers all these solutions with just one set of tools.
Contact us to learn how ESHs can improve your shop floor's production efficiency.